
EN Contact Us
Engineered for high thermal conductivity, electromagnetic shielding (EMI/RFI), and severe environment resistance across Chicagoland’s manufacturing sector.
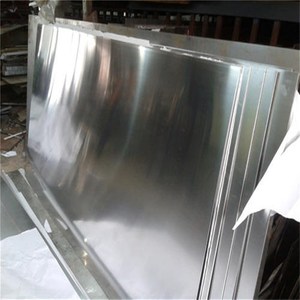
Direct-cast (DC) heavy-duty aluminum plates engineered for structural NEMA 4X electrical cabinets. Features extreme resistance to Midwest de-icing salts and industrial chemicals.
Contact Us
Full spectrum 6061-T6, 7075-T6, and 5052-H32 cut-to-size plate stock. Designed for deep CNC milling of power electronics chassis, heat-sink housings, and structural side panels.
Contact Us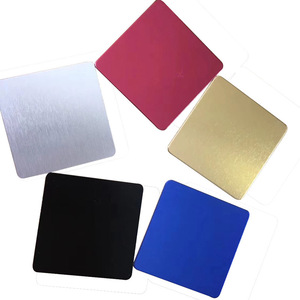
Type II sulfuric anodized decorative panels in Gold, Black, Blue, and Silver. Provides dielectric insulation, high scratch resistance, and premium surface aesthetic for rack units.
Contact Us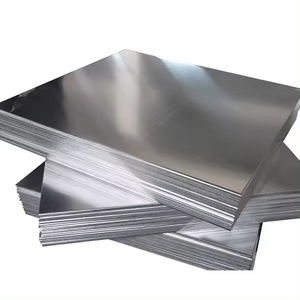
Certified marine-grade structural aluminum sheets optimized for Lake Michigan waterfront telemetry, municipal infrastructure, and sub-zero freeze-thaw transit control boxes.
Contact Us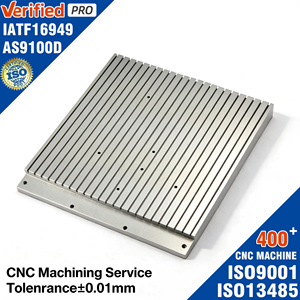
5-axis precision CNC milled 6061-T6 aluminum enclosure shells. Features embedded cooling fins, O-ring gasket channels, and conductive surface treatments for aerospace rigor.
Contact Us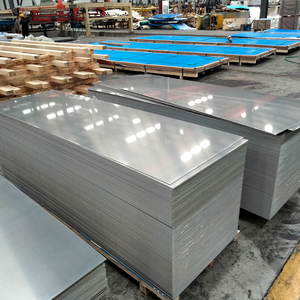
High-ductility aluminum alloy stock ideal for brake pressing, seam welding, and deep-drawing into seam-free NEMA 12 and NEMA 3R outdoor industrial automation cabinets.
Contact Us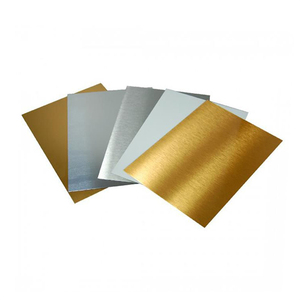
Satin-finish electrolytic anodized plates developed for medical equipment enclosures, food processing control interfaces, and sterile environment monitoring stations.
Contact Us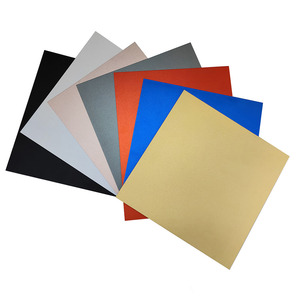
Ultra-thin, precision-stamped aluminum foil sheets designed as internal electromagnetic interference (EMI) shields, membrane switch backplates, and lightweight thermal baffles.
Contact UsA technical guide to alloy selection, thermal management physics, NEMA protection, and domestic supply chain optimization.
As Chicagoland solidifies its position as the premier Midwest nexus for advanced robotics, food processing automation, heavy machinery, and smart grid power distribution, the demand for high-performance custom aluminum enclosures has evolved beyond off-the-shelf catalog boxes. Modern industrial electronics generate unprecedented heat flux density while operating in harsh environments ranging from sub-zero outdoor weather in Northern Illinois to high-pressure chemical washdowns in food manufacturing facilities.
Choosing the correct aluminum enclosure factory involves understanding the interplay between chemical alloy composition, mechanical grain structure, thermal dissipation capabilities, and environmental sealing standards (NEMA 250 and IEC 60529 IP ratings). This white paper provides an authoritative analysis of custom aluminum enclosure engineering for engineering directors, procurement managers, and system integrators across Greater Chicago.
Aluminum is specified over carbon steel and stainless steel in high-reliability applications due to its superior strength-to-weight ratio, native passivation oxide layer, high thermal conductivity (160 to 200 W/m·K vs. 16 W/m·K for 304 stainless steel), and excellent electromagnetic shielding efficiency. However, selecting the precise alloy and temper dictates long-term performance:
| Alloy Grade | Temper | Tensile / Yield (MPa) | Thermal Cond. (W/m·K) | Corrosion Resistance | Optimal Chicago Application |
|---|---|---|---|---|---|
| 6061 | T6 / T651 | 310 / 276 | 167 | High (Atmospheric) | Heavy CNC Machined Chassis, Electronics Housings, High-Stress Frame Modules |
| 5083 | H116 / H321 | 305 / 215 | 120 | Exceptional (Marine/Salt) | Lake Michigan Waterfront Systems, De-Icing Chemical Exposure, Municipal Transit |
| 5052 | H32 / H34 | 230 / 193 | 138 | Excellent (Industrial) | Sheet Metal Cabinets, Deep-Drawn Enclosures, NEMA 4X Washdown Boxes |
| 7075 | T6 / T6511 | 572 / 503 | 130 | Moderate (Protected) | Aerospace Ground Support, High-Impact Military Enclosures, Defense Electronics |
| 3003 | H14 / H18 | 160 / 145 | 193 | Good (General) | Heat Exchanger Shells, Thin-Gauge Foil Liners, Formed Electronic Cover Plates |
For structural load-bearing cabinets subject to high vibration—such as rail transit controllers along the CTA corridors or heavy stamping presses in Rockford—Alloy 6061-T6 offers high yield strength and dimensional stability during aggressive 5-axis CNC machining. Conversely, for sheet metal enclosures requiring intricate brake-press forming and seam-welding without micro-cracking, Alloy 5052-H32 provides exceptional ductility and work-hardening characteristics.
Enclosure thermal management is a primary point of failure for sealed industrial drive units and PLC control racks. Sealing an enclosure to NEMA 4X or IP66 standards prevents dust and jet-directed washdown water from entering, but it also traps internally generated heat. Heat transfer occurs via three mechanisms:
By engineering internal liquid cold plates (utilizing high-purity 3003 or 6061 extruded flow channels) and integrating external cooling fins directly into the enclosure's structural sidewalls, heat dissipation surface area can be increased by up to 320% compared to smooth-walled steel enclosures. This allows high-density electronics to run 15°C to 25°C cooler, exponentially extending component mean time between failures (MTBF).
A critical consideration for Chicago-area buyers is protecting metal enclosures against aggressive seasonal ambient conditions—ranging from high summer humidity along Lake Michigan to road salt mist during harsh Midwest winters. Our in-house surface finishing suite includes:
Custom-engineered aluminum enclosures tailored specifically to the regional operating demands of Northern Illinois and Midwest industrial corridors.
Corridor Focus: Fulton Market, Stockyards Industrial Corridor, and Elgin Food Plants.
Environments requiring daily high-pressure washdown at 1,500 PSI using caustic sodium hydroxide solutions. Our 5052-H32 seam-welded NEMA 4X enclosures feature continuous smooth welds, rounded hygienic corners, and chemical-resistant EPDM gasket channels that eliminate bacterial harborage points.
Corridor Focus: O'Hare Logistics Belt, Elk Grove Village, and Bolingbrook Hubs.
High-acceleration automated guided vehicles (AGVs) and sorting robotics require lightweight, ultra-rigid chassis enclosures. Our AS9100-certified CNC milled 6061-T6 aluminum shells reduce robotic arm payload inertia by up to 60% compared to sheet steel, increasing battery life and cycle speed.
Corridor Focus: Substation Retrofits, Chicagoland Solar Parks, and EV Charging Stations.
Outdoor power electronics subjected to -30°C winter cold and +40°C summer heat. Utilizing thermal break aluminum extrusions and high thermal mass 6061-T6 heat spreader plates, our cabinets prevent internal condensation while ensuring battery thermal runaway protection.
Why Midwest OEM engineering teams are transitioning from imported off-the-shelf boxes to factory-direct custom aluminum enclosures.
The industrial landscape of the Midwestern United States is undergoing a major transformation. Three key macro trends are re-shaping how Chicago companies procure custom electronic and electrical enclosures:
Historically, many North American buyers relied on standard overseas catalog suppliers for stamped steel junction boxes. However, lead time uncertainty, unpredictable ocean freight surcharges, and high minimum order quantities (MOQs) have exposed vulnerabilities in off-shore sourcing strategies. By partnering directly with a fully integrated aluminum extrusion and precision CNC machining factory capable of handling custom die creation, rapid prototyping, and finished assembly under one roof, Chicago buyers can shorten product launch cycles from 24 weeks down to 15 to 20 working days.
Weight reduction is no longer confined to aerospace. Heavy equipment manufacturers in Aurora, Peoria, and Quad Cities are actively re-engineering structural machine enclosures to replace heavy, rust-prone carbon steel with high-strength 5083 and 6061 aluminum alloy plates. Aluminum is 100% infinitely recyclable without material degradation. Recycling aluminum requires only 5% of the energy consumed in primary metal production, allowing Midwest OEMs to meet stringent scope 3 carbon reduction mandates.
With the deployment of 5G industrial private networks, smart manufacturing facilities in Schaumburg and Rockford require edge-computing enclosures installed directly on the factory floor. These compute units generate significant high-frequency electromagnetic noise (RFI) and substantial heat. Custom aluminum enclosures featuring conductive trivalent chromate conversion coatings and integrated EMC shielding gaskets satisfy FCC Class A radiation compliance while acting as giant passive heat exchangers.
Backed by over five decades of metallurgical experience, state-of-the-art multi-press extrusion lines, and complete in-house fabrication.
Unlike distributor intermediaries or assembly-only job shops, our manufacturing facility controls every link of the production chain:
Clear, direct technical responses to common procurement, engineering, and shipping questions.
We primarily extrude and machine 6063-T5/T6 for extruded profiles and heat sink walls, 6061-T6/T651 for high-strength CNC machined structural chassis, 5052-H32 for sheet metal formable cabinets, and marine-grade 5083-H116 for severe washdown or salt-mist environments. Alloy certificates and Mill Test Reports (MTRs) tracing heat chemistry accompany every shipment.
Both materials fulfill NEMA 4X corrosion and washdown requirements. However, 5052 or 5083 aluminum enclosures offer three key advantages over 304/316 stainless steel: they are roughly one-third the weight, provide dramatically higher thermal conductivity (preventing hot spots inside the box), and are substantially more cost-effective to precision machine and cut on CNC equipment.
For custom extruded aluminum enclosure profiles, new die creation typically takes 10 to 15 working days. Once the die is completed, first-article sample profiles are extruded, machined, and inspected for dimensional compliance. Bulk production runs typically ship within 2 to 3 weeks following your written sample approval.
For outdoor enclosures installed in Chicagoland, we recommend an architectural polyester powder coat (minimum 60–80 microns film thickness) applied over a chromate-free pre-treatment line, or a Type III Hardcoat Anodize (50 microns). Both finishes withstand freeze-thaw thermal cycling and prevent salt pitting from highway de-icing compounds.
Because we operate our own extrusion presses and CNC milling lines, our MOQs are flexible. Standard MOQ for custom extruded profiles starts at 500 kg to 1,000 kg per run. For fully CNC-machined plate enclosures or prototypes, we support low-volume pre-production batches (10–50 units) up to high-volume recurring OEM production runs.
All finished enclosures, panels, and extruded components are wrapped with interleaved protective polyethylene film or anti-abrasion kraft paper. Bundles are strapped onto heavy-duty heat-treated timber pallets (ISPM-15 compliant) with corner edge-protectors, fully prepared for LTL or full-container transport directly to your Chicago facility or jobsites.
Send your CAD drawings (.STEP, .DXF, .DWG) or physical samples to our engineering team today for a comprehensive design-for-manufacturability (DFM) review and competitive factory-direct quote.
Contact Us