
EN Contact Us
Engineered to ASTM B209, EN 573, and ISO 9001:2015 specifications. Direct mill allocation for global enterprise fabricators, marine shipbuilders, and precision machining facilities.
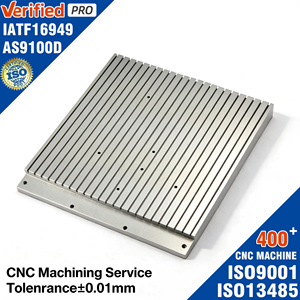
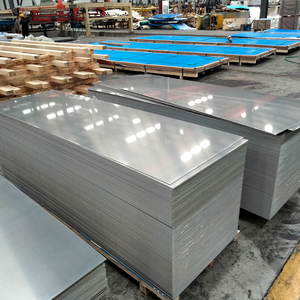
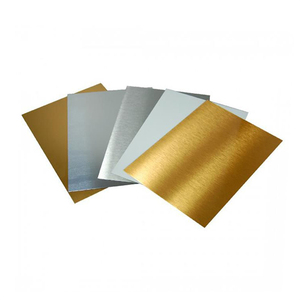
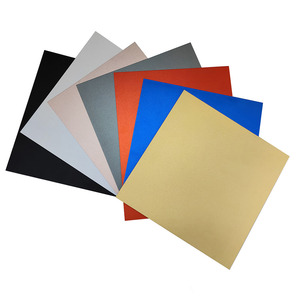
In the contemporary global manufacturing ecosystem, primary aluminum ingots, foundry alloy remelt ingots (RSI), and extruded billets form the foundational bedrock for automotive lightweighting, structural aerospace engineering, electrical infrastructure, solar PV frame fabrication, and architectural facade engineering. Procuring commercial aluminum ingots requires far more than comparing spot market pricing against London Metal Exchange (LME) benchmarks. It necessitates a rigorous technical evaluation of primary smelting methodologies, spectrographic impurity thresholds, melt degassing standards, and supply chain decarbonization metrics.
As a tier-1 integrated metallurgical group tracing its roots back to 1972, our enterprise operates across the entire non-ferrous value chain—combining continuous casting, electromagnetic induction refining, automated extrusion, and advanced surface finishing within a unified quality management framework. This white paper serves as an authoritative procurement directive for Chief Procurement Officers (CPOs), metallurgical engineers, and industrial buyers seeking to mitigate procurement risk, optimize chemical purity tolerances, and secure long-term alloy stability.
Aluminum ingots are classified according to their chemical composition, smelting process, and downstream fabrication intent. Understanding these distinction boundaries prevents costly casting porosity, cracking, and mechanical performance failures during downstream processing:
| Ingot Grade / Alloy Designation | Al Purity / Primary Elements | Max Fe Content | Tensile Strength (MPa) | Primary Industrial Application |
|---|---|---|---|---|
| P1020A (Standard Primary) | ≥ 99.70% Al | 0.10% | 70 - 90 (As Cast) | Electrical Conductor Rods, Remelt Base, Foil Stocks |
| High Purity A8 (P0610) | ≥ 99.85% Al | 0.06% | 75 - 95 (As Cast) | Specialty Chemical Vessels, Anodizing Stock, Optical Alloys |
| A356.2 Foundry Ingot | Si 6.5-7.5%, Mg 0.30-0.45% | 0.12% | 220 - 310 (T6 Condition) | Automotive Wheels, Structural Aerospace Castings |
| ADC12 / A380 Foundry Ingot | Si 9.6-12.0%, Cu 1.5-3.5% | 0.90% | 310 - 330 (Die Cast) | Machinery Covers, Automotive Powertrain Gear Cases |
| 6061 DC Extrusion Billet | Mg 0.8-1.2%, Si 0.4-0.8% | 0.70% | 290 - 310 (T6 Temper) | Structural Bridges, Rail Cars, CNC Machining Components |
| 7075 Aerospace Billet/Slab | Zn 5.1-6.1%, Mg 2.1-2.9% | 0.50% | 540 - 570 (T651 Temper) | Defense Framing, Aerospace Spars, High-Stress Mold Tooling |
Operating seamlessly under a family metals group with continuous metallurgical operations since 1972, HAQ Aluminium represents over 53 years of industrial leadership across scrap refining, billet casting, structural extrusion, and surface treatment. Spanning a 650-strong workforce in Lahore, Pakistan, our facilities incorporate in-house optical emission spectrometers (OES), rotary degassing units using Argon-Chlorine gas mixtures, and two-stage 30-ppi ceramic foam filters.
This comprehensive internal oversight ensures that every heat cast into ingots or extruded into high-precision structural plates—ranging from marine-grade 5083/5754 to aerospace-grade 7075 T651—exhibits absolute chemical homogeneity, zero internal hydrogen porosity (≤ 0.12 cm³/100g Al), and complete freedom from non-metallic inclusions.
The next decade of B2B non-ferrous metal procurement will be characterized by extreme price volatility, stringent environmental regulations, and automated quality auditing. Enterprise procurement teams must realign their sourcing strategies around four core macro trends:
Global buyers are shifting away from static fixed-rate pricing toward dynamic LME + Regional Ingot Premium contracts. Utilizing cash-settled futures, Asian physical premiums (MJP), and European Duty-Paid premiums allows procurement managers to hedge raw material exposure while locking in processing margins 6 to 12 months in advance.
With cross-border carbon tariffs expanding across North America and Europe, verified "Green Aluminum" (ingots produced via hydroelectricity or scrap-rich secondary smelting with ≤ 4.0 CO2/kg Al) commands a distinct structural advantage, reducing long-term regulatory compliance liabilities.
Automotive OEMs are enforcing closed-loop circular sourcing. Modern smelters blend primary P1020 liquid aluminum with up to 30-50% clean pre-consumer industrial scrap, utilizing electromagnetic induction furnaces to match standard prime alloy strength while drastically lowering embodied energy by 95%.
The global consumption of specialized aluminum ingots and rolled plate products is undergoing exponential demand shifts driven by two key industry verticals:
Electric Vehicle (EV) Structural Chassis & Battery Enclosures: The transition from internal combustion engines (ICE) to EV architectures requires high-energy absorption structural alloys. Castings made from low-iron A356-T6 foundry ingots and 6061/7075 extrusions enable complex single-piece gigacastings, reducing vehicle kerb weight by up to 30% and directly extending battery range.
Renewable Energy PV Framing & Tracker Rail Infrastructure: Utility-scale solar installations rely heavily on anodized 6060, 6063, and 6005A alloy extrusions. High-purity billets with controlled micro-alloying elements (Titanium and Boron grain refiners) prevent premature fatigue cracking under extreme wind loads and corrosive desert or offshore salt-spray environments.
Direct technical clarity for B2B procurement officers, casting engineers, and international metal buyers.
Standard P1020 aluminum ingots adhere to ISO 1156 and GB/T 1196-2017 standards, specifying a minimum aluminum purity of 99.70%. The maximum iron (Fe) threshold is capped strictly at 0.10%, and silicon (Si) is capped at 0.10%. For more demanding applications such as high-reflectivity lighting or specialty anodizing plate alloys, high-purity P0610 (A8) ingots with Fe ≤ 0.06% are recommended.
Molten aluminum readily absorbs hydrogen gas during smelting and transfer. If not purged, dissolved hydrogen forms microscopic gas porosity during solidification, leading to structural weakness and pressure test failures. Our processing involves inline rotary degassing injection using high-purity Argon gas mixed with trace Chlorine, reducing hydrogen concentrations below 0.12 cm³/100g Al, verified via reduced pressure test (RPT) density measurements.
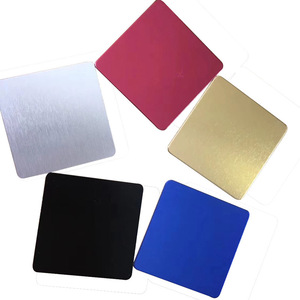
We supply aluminum plates and sheets in Mill Finish, Electrostatic Architectural Polyester Powder Coating (RAL color matching), Color Anodized finishes (Gold, Black, Blue, Silver, Bronze at 10-25 micron film thicknesses), Brushed Mechanical Finishes, and PVDF Fluorocarbon coatings designed for 20+ year exterior building envelope warranties.
Yes. Utilizing state-of-the-art medium-frequency induction melting furnaces and spectrographic verification, custom foundry master alloys can be blended to exact customer drawings or chemical range limits. Minimum custom melt batch sizes typically range from 5 to 10 metric tons, accompanied by a mill Certificate of Analysis (COA) per ladle.
Aluminum ingots are bundled in steel or heavy-duty plastic strapping (approx. 500 kg to 1,000 kg per stack) on fumigated wooden skids or aluminum runners. Plates and cut sheets are interleaved with neutral pH protective paper or PE protective film, wrapped in moisture-proof plastic barriers, desiccated, and enclosed in seaworthy wooden crates designed for 20ft/40ft container shipping.
International aluminum pricing uses the formula: Total Price = LME Cash Settlement Price + Physical Regional Premium (e.g., MJP / Rotterdam Duty Paid) + Specific Smelting/Alloy Fabrication Charge. Pricing can be locked via spot contract upon deposit or indexed to the average monthly LME cash price during the bill-of-lading (MOM) period.
Request custom alloy quotations, direct mill allocation schedules, Certificate of Analysis (COA) documentation, or technical drawing evaluations today.