
EN Contact Us
Direct mill-to-market custom extruded sections, high-precision alloy plates, and architectural finishing systems tailored for global procurement requirements.
Marine-grade alloy, superior stress-corrosion resistance, custom cut-to-length dimensions.
Send an Inquiry
Wide gauge versatility, high structural strength, certified tolerance limits for industrial OEMs.
Send an Inquiry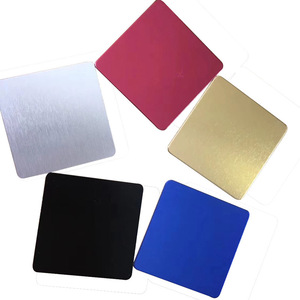
Electrochemically sealed oxide film, consistent color batch control, scratch-resistant finish.
Send an Inquiry
DNV/ABS compliant marine structural sheet, engineered for severe salt-water environments.
Send an Inquiry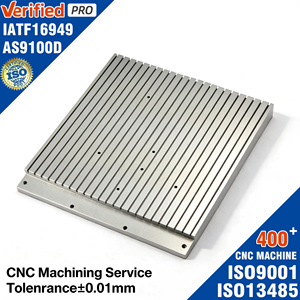
Aerospace and machinery grade tight-tolerance milling, drilling, turning, and profiling.
Send an Inquiry
Zero internal tension, flat-plate technology for high-speed automated processing lines.
Send an Inquiry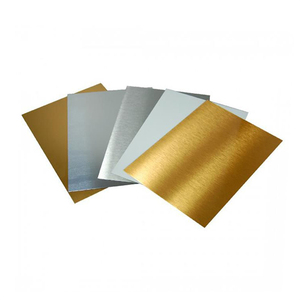
High-aesthetic industrial enclosure plates with UV-stabilized organic organic dye sealing.
Send an Inquiry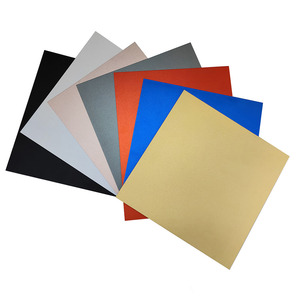
Flexible shim and trim stock, precision stamped for electronics, decoration, and heat shields.
Send an InquiryIn modern industrial engineering, aluminum profile extrusion represents the cornerstone of lightweight structural design, thermal management, and architectural innovation. As global supply chains shift toward carbon-neutral materials and strict dimensional repeatability, B2B buyers require complete clarity regarding the extrusion lifecycle—from raw primary ingot chemistry to final post-machining surface passivation.
Original Equipment Manufacturers (OEM) and Original Design Manufacturers (ODM) face mounting pressure to balance high strength-to-weight ratios with tight geometric tolerances. Standard off-the-shelf extrusions frequently fail under dynamic wind loads, harsh marine salt spray, or extreme thermal cycling. Partnering with a fully integrated OEM/ODM extruder eliminates third-party handovers, reducing lead times from die development to container loading while maintaining strict traceabilities across alloy batches.
The metallurgical integrity of an extruded profile is governed by the quality of the starting billet. Utilizing 100% primary aluminum ingot homogenized at precise temperatures (560°C–580°C) ensures an even distribution of alloying elements like Magnesium (Mg) and Silicon (Si). This eliminates coarse Mg₂Si phase precipitates, preventing premature die stress, wall tearing, and inconsistent anodizing responses.
Choosing the correct aluminum alloy temper is a critical procurement decision. A common failure mode in custom profile sourcing is specifying a decorative alloy for a load-bearing structural application, or selecting a non-heat-treatable alloy for high-stress CNC components. Below is a detailed engineering comparison of standard OEM/ODM extrusion and plate alloys:
| Alloy Series | Primary Temper | Tensile Strength (MPa) | Yield Strength (MPa) | Corrosion Resistance | Primary B2B Application |
|---|---|---|---|---|---|
| 6063 | T5 / T6 | 150 – 240 | 110 – 200 | Excellent | Architectural windows, doors, curtain walls, thermal break profiles |
| 6061 | T6 / T651 | 290 – 310 | 240 – 275 | Very Good | Structural frameworks, transport chassis, industrial machine automation |
| 6082 | T6 | 310 – 340 | 260 – 290 | Very Good | High-stress structural beams, bridges, crane girders, marine superstructures |
| 5083 / 5754 | H111 / H116 / H321 | 270 – 350 | 125 – 220 | Superior (Saltwater) | Shipbuilding, pressure vessels, vehicle bodies, chemical tank storage |
| 7075 | T6 / T651 | 530 – 570 | 460 – 500 | Fair | Aerospace fittings, high-stress military components, precision CNC tooling |
For structural architectural profiles, 6063-T5/T6 remains the industry standard due to its smooth surface finish and rapid extrusion speeds. However, for heavily loaded solar panel framing or industrial liquid cold plates, shifting to 6061-T6 or 6082-T6 provides up to a 45% increase in yield strength without sacrificing extrudability.
Our fully integrated facility combines die engineering, multi-press extrusion lines, fully automated vertical powder coating, and 5-axis CNC post-machining under one Quality Management System.
In-house CAD/CAM toolroom capable of sinking custom steel dies from 2D DXF or 3D STEP models. Standard tooling lead times range from 10 to 15 working days, accompanied by full First Article Inspection Reports (FAIR).
Multiple press lines ranging from 600 Tons to 3,600 Tons force. Capable of extruding solid, semi-hollow, and complex hollow sections with circumscribing circle diameters up to 350mm.
In-house architectural powder coating (Qualicoat standard), Class I/II anodizing (10–25 microns), electro-phoretic painting, and high-fidelity wood-grain sublimation thermal transfer.
Post-extrusion value-add services including 3-axis and 5-axis CNC milling, high-speed tapping, precision miter cutting, stamping, punch press slotting, and robotic welding assemblies.
As international environmental regulations tighten, procurement leaders must look beyond raw unit cost per kilogram. Semantic procurement data indicates three major macro-trends shaping B2B extruded profile sourcing over the next decade:
Global buyers are demanding certified low-carbon aluminum billets. Utilizing scrap recycling within closed-loop manufacturing cuts energy consumption by up to 95% compared to primary smelting. European and North American buyers are increasingly enforcing Carbon Border Adjustment Mechanisms (CBAM), requiring suppliers to provide detailed Environmental Product Declarations (EPD).
With global green building codes requiring ultra-low U-values in curtain wall facades and residential glazing systems, single-wall solid extrusions are being replaced by polyamide strip thermal break assemblies (PA66 GF25). Mechanically crimping structural fiberglass-reinforced polyamide strips between inner and outer aluminum channels dramatically eliminates conductive thermal bridging.
The explosive growth in Electric Vehicle (EV) battery enclosures and photovoltaic (PV) inverter solar mounting systems has accelerated demand for complex thin-wall multi-void profiles. Heat sink extrusions require high fin-to-base ratios (up to 15:1) to dissipate thermal loads efficiently without adding excess vehicle mass.
A major risk in international profile procurement is dimensional distortion caused by improper cooling quenches or internal residual stress. To guarantee structural integrity upon delivery, our quality control procedures rigorously enforce international testing benchmarks:
Automated Optical CMM profile projectors verify wall thickness, corner radius, twist, bow, and angularity against EN 12020-2 / ASTM B221 tolerance standards.
Destructive testing verifies ultimate tensile strength (UTS), yield strength (YS), and percentage elongation for every artificial ageing batch (T5/T6).
Cross-hatch tape adhesion (ISO 2409) and 1,000+ hour neutral salt spray (ASTM B117) tests verify zero film blistering or filiform corrosion under extreme exposure.
With over five decades of deep metallurgical legacy dating back to 1972, our enterprise has evolved from foundational metal trading into a fully integrated global manufacturing leader in architectural systems and industrial extrusions.
Direct engineering answers to common technical queries regarding custom extrusion orders.
Submit your 2D/3D profile drawings or product specifications today. Our engineering team provides extrudability analysis, tooling estimates, and formal B2B price quotes within 24 business hours.
Send an Inquiry