Technical Specification & Metallurgy of Custom Extruded OEM Aluminum Bars
In modern industrial manufacturing, the demand for high-integrity structural materials has driven custom OEM aluminum bar procurement to unprecedented technical heights. Extruded aluminum bars—encompassing round, square, rectangular, and custom geometric cross-sections—serve as the foundational backbone for automotive lightweighting, structural building curtain walls, renewable energy solar framing, and precision CNC-machined components.
Achieving optimal mechanical properties requires a deep understanding of alloy chemistry, billet homogenization, extrusion press dynamics, thermal quenching, and artificial precipitation hardening (aging). B2B procurement managers and engineering executives must look beyond surface-level pricing to evaluate the core metallurgical parameters that govern real-world performance.
Chemical Composition & Mechanical Property Matrix
Selecting the correct aluminum alloy temper is the most critical decision in product engineering. The table below outlines the primary industrial alloys utilized in custom OEM bar manufacturing and export supply chains:
| Alloy Standard |
Temper Class |
Tensile Strength (MPa) |
Yield Strength (MPa) |
Elongation (%) |
Primary Application Fields |
| 6063 |
T5 / T6 |
205 - 245 |
170 - 210 |
8 - 12 |
Architectural trim, window framing, heat sinks, conduit profiles. |
| 6061 |
T6 / T6511 |
290 - 310 |
240 - 275 |
10 - 17 |
Structural frames, truck beds, marine deck bars, precision CNC parts. |
| 6082 |
T6 |
310 - 340 |
260 - 290 |
8 - 10 |
High-stress structural bridges, cranes, trusses, transport machinery. |
| 5083 |
H111 / H116 |
275 - 350 |
125 - 200 |
12 - 16 |
Marine vessel hulls, cryogenics, pressure vessels, chemical tanks. |
| 7075 |
T6 / T651 |
540 - 570 |
470 - 500 |
7 - 11 |
Aerospace spars, defense hardware, high-fatigue structural tooling. |
To guarantee that these mechanical properties are consistently met, advanced OEM factories employ direct-chill (DC) casting to produce dense, gas-free aluminum billets. Billet homogenization at temperatures exceeding 560°C eliminates dendritic segregation, ensuring uniform grain structure throughout the solid profile during extrusion.
Future Procurement Trends in the Global Aluminum Bar Market (2025–2030)
The global aluminum sourcing landscape is undergoing a systemic transition driven by environmental regulation, supply chain regionalization, and technological integration. Purchasing directors and global trade buyers must align their procurement strategies with four key emerging trends:
1. Decarbonization & Low-Carbon "Green Aluminum" Mandates
With the implementation of the European Union's Carbon Border Adjustment Mechanism (CBAM) and global ESG compliance frameworks, the carbon footprint of raw aluminum has become a commercial differentiator. Primary aluminum smelted using hydro-electric power produces under 4.0 kg CO2 per kg of aluminum, compared to fossil-fuel-derived smelting which can generate up to 20.0 kg CO2 per kg. Leading OEM exporters are incorporating recycled scrap (post-industrial closed-loop recycling) directly into their log re-melting furnaces, reducing energy consumption by up to 95% while retaining full alloy performance.
2. Digital Twin Die Design & Automated Simulation
Traditional trial-and-error die testing is rapidly being replaced by finite element analysis (FEA) and computational fluid dynamics (CFD) extrusion simulation software. Modern OEM exporters use digital twin technology to predict metal flow velocity, thermal gradients, and die deflection before cutting physical steel. This reduces die correction cycles from 4-5 iterations down to a single pass, enabling 10-day die turnover times and dramatically cutting NRE (Non-Recurring Engineering) tooling costs for buyers.
3. Near-Net-Shape Extrusion & CNC Machining Integration
Global buyers are increasingly abandoning raw mill-finish bar stock in favor of "fabrication-ready" components. OEM exporters that integrate extrusion presses directly with 5-axis CNC machining centers, automated double-head saws, and robotic welding cells offer significant landed-cost savings. By purchasing near-net-shape bars cut, drilled, chamfered, and surface-treated at the factory level, overseas buyers eliminate domestic scrap waste, reduce freight bulk weight, and streamline assembly lines.
4. Blockchain-Backed Material Traceability
Supply chain transparency has become non-negotiable for Tier-1 automotive, aerospace, and defense contractors. Advanced aluminum bar factories now bind spectroscopic chemical test logs, ultrasonic flaw detection scans, and heat-treatment chart curves to unique QR-coded bundle tags. This digital passport allows buyers to trace finished aluminum bars directly back to the exact primary smelting heat lot.
Development Trends in Extrusion Technology & Surface Finishing
As end-use applications demand tighter tolerances and longer service lifetimes in aggressive environments, manufacturing technology continues to advance across three main vectors:
Microstructural Engineering & Water-Air Dual Quenching
For high-strength 6000-series alloys, the rate of temperature drop immediately after exiting the extrusion die container determines precipitation behavior. Modern high-speed extrusion lines utilize computerized dual water-spray and high-velocity air quench systems. Rapid cooling traps Mg2Si (magnesium silicide) phase elements in solid solution, allowing subsequent artificial aging ovens to achieve uniform T6 hardness without inducing thermal distortion along the length of long bar profiles.
Chromate-Free Eco-Friendly Pre-Treatment & Advanced Anodizing
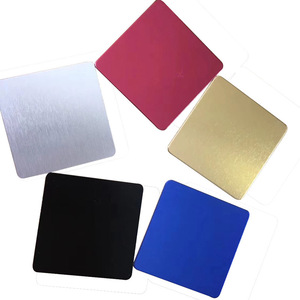
Environmental standards have led to the complete phase-out of hexavalent chromium pre-treatments. Today's leading OEM factories utilize zirconium-titanium chemical conversion coatings. This produces an nano-ceramic adhesion layer that increases powder coat paint bonding strength to over 5B (ASTM D3359) while resisting over 3,000 hours of neutral salt spray testing (ASTM B117). Furthermore, electro-chemical hard-coat anodizing capabilities now produce oxide layers exceeding 25 microns, offering surface hardness levels comparable to hardened tool steel.
Precision Straightening & Low-Stress Stretch Tensioning
Post-extrusion thermal stress can induce bow and twist in solid aluminum bars. Advanced hydraulic stretchers with automatic load-cell feedback exert precise elongation tensioning (typically 1.0% to 1.5% permanent stretch). This process releases internal residual stress, ensuring that when the aluminum bar stock is subsequently milled or slotted on high-speed CNC machines, it does not warp or spring out of linear tolerance.