
EN Contact Us
The global industrial landscape for custom metal components has underwent a fundamental transformation. Driven by stringent carbon-reduction targets, rapid vehicle electrification, and high-density electronic packaging requirements, global original equipment manufacturers (OEMs) and tier-1 procurement networks demand more than basic production capabilities. Sourcing high-precision aluminum casting parts from China has evolved from a pure cost-arbitrage leverage point into a strategic partnership centered on material science, Design for Manufacturability (DFM), and integrated 5-axis CNC machining capabilities.
China's aluminum casting foundry sector represents over 55% of global output, boasting an unparalleled supply chain density. Modern Chinese foundry operations seamlessly integrate high-pressure die casting (HPDC), low-pressure die casting (LPDC), gravity sand casting, and investment lost-wax processes with automated robotic cells and real-time process monitoring. This technical whitepaper explores the critical engineering parameters, alloy selection criteria, procurement roadmaps, and technological vectors that define world-class OEM/ODM aluminum die casting suppliers in China.
Engineered to exact drawing specifications with high-repeatability die casting molds and in-house multi-axis CNC finishing
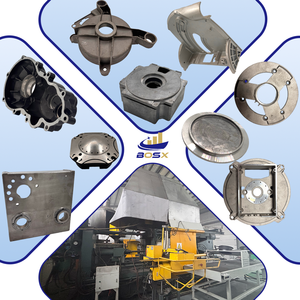
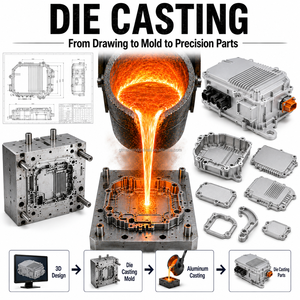
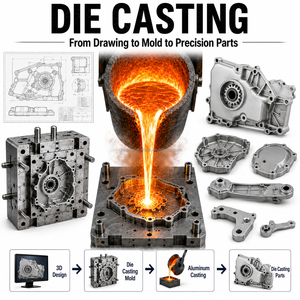
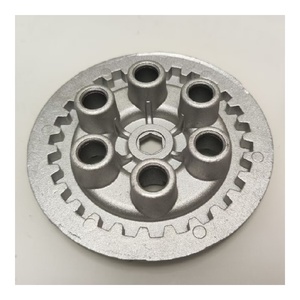
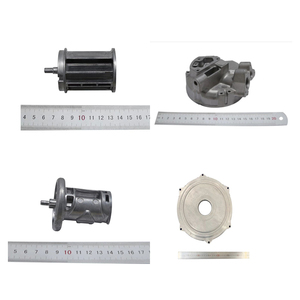
A comparative analysis of aluminum casting methods, material performance specs, and structural tolerances
Selecting the optimal casting process is a multi-objective optimization problem involving mechanical strength, thermal conductivity, surface roughness, part complexity, annual volume, and initial tooling expenditure. Premier Chinese export foundries operate across four primary aluminum casting methodologies, each matched to specific alloy chemical compositions.
| Casting Process | Typical Alloys Used | Tolerance Range | Min Wall Thickness | Surface Finish (Ra) | Economic Volume |
|---|---|---|---|---|---|
| High Pressure (HPDC) | A380, ADC12, A360 | ±0.05 mm – ±0.1 mm | 1.2 mm | 1.6 – 3.2 μm | > 3,000 pcs / year |
| Low Pressure (LPDC) | A356, A357, ZL101A | ±0.15 mm – ±0.3 mm | 2.5 mm | 3.2 – 6.3 μm | > 1,000 pcs / year |
| Investment Casting | A356, AlSi10Mg, 6061 | ±0.02 mm – ±0.08 mm | 1.0 mm | 0.8 – 1.6 μm | 100 – 2,000 pcs / year |
| Gravity Sand Casting | A356, ZL104, ZL102 | ±0.4 mm – ±0.8 mm | 4.0 mm | 6.3 – 12.5 μm | 1 – 500 pcs / year |
Complete in-house value chain control from initial mold DFM simulation to high-precision 5-axis CNC finishing and international compliance
Integrated toolmakers leverage CAD/CAM software (MAGMAsoft mold flow, SolidWorks, UG NX) to design hardened H13/DIEVAR steel dies. Enables rapid 10–15 day die sinking, minimizing gas porosity and thermal fatigue.
Over 100 high-speed 5-axis and 4-axis CNC machining centers equipped with automatic tool changers and probing systems deliver precise hole-to-hole centerlines, milled face flatnesses, and micro-tolerances down to ±0.02 mm.
Rigorous quality protocols utilizing Zeiss Coordinate Measuring Machines (CMM), optical emission direct-reading spectrometers, non-destructive X-ray flaw detectors, ultrasonic porosity testing, and helium leak detectors.
Key technological disruptions reshaping OEM supply chains and supplier selection criteria over the next decade
As international supply chains emphasize decarbonization, total cost of ownership (TCO), and accelerated time-to-market, procurement teams must evaluate manufacturers against emerging technological benchmarks. The future of China wholesale aluminum casting lies in the convergence of automated foundry hardware, green metallurgy, and digital quality monitoring systems.
The automotive sector is moving toward replacing multi-part stamped assemblies with single-piece, ultra-large die castings. Presses ranging from 6,000 to 12,000 tons cut assembly line footprints, eliminate hundreds of weld points, and enhance structural frame rigidity. Leading Chinese foundries are investing heavily in mega-die tooling infrastructure to support next-generation EV platforms.
Decarbonization mandates require suppliers to offer secondary aluminum alloys with high recycled scrap content (exceeding 80–90%) without sacrificing mechanical yield strength or ductility. Advanced degasification, electromagnetic stirring, and precise ceramic filtration systems allow foundries to produce premium structural castings with a 90% reduced embedded carbon footprint.
Eliminating air entrapment during shot sleeve injection is essential for parts undergoing subsequent T6 heat treatment or structural welding. High-vacuum die casting systems reduce cavity pressure below 30 mbar prior to liquid metal injection, virtually eliminating micro-porosity and enabling leak-proof performance for heat exchangers and hydraulic valve blocks.
Top-tier Chinese manufacturers now use generative AI algorithms coupled with finite element thermal analysis (FEA) during the initial drawing phase. This simulates thermal stress points, solidification shrinkage, and turbulent mold filling before steel is cut, reducing prototype iterations from months to days.
Detailed technical guidance addressing key commercial, metallurgical, and logistics inquiries
For applications exposed to salt spray, humidity, or harsh chemicals, A356.0 or AlSi10Mg modified alloys subjected to Type II or Type III (Hardcoat) anodizing are recommended. These alloys feature low copper content (<0.1% Cu), drastically mitigating galvanic corrosion risks compared to standard die casting grades like A380 or ADC12.
Leading exporters utilize a multi-tier quality protocol: high-efficiency vacuum degassing units prior to pouring, real-time ceramic foam filtration, high-vacuum assisted die cavity evacuation during injection, and 100% non-destructive X-ray flaw inspection on critical cross-sections to verify density.
Standard die casting mold design, DFM flow simulation, CNC tool sinking, and initial T1 sample delivery typically take 15 to 25 calendar days depending on tool complexity, slide mechanisms, and core pull requirements. First Article Inspection (FAI) reports with complete CMM dimensional scans are supplied with sample shipments.
Full turnkey finishing options include shot/sand blasting, vibratory deburring, CNC precision milling, anodizing (clear, color, hardcoat), electrostatic powder coating (RAL color matching, architectural grade), chromate conversion coatings (RoHS/REACH compliant Alodine), E-coating (electrophoretic painting), and laser marking.
Production MOQs generally range from 500 to 1,000 units depending on part weight and press tonnage requirements. For export shipments, parts are wrapped in anti-corrosion VCI (Volatile Corrosion Inhibitor) film, placed in customized partition foam trays, and packed inside reinforced ISPM-15 heat-treated fumigated wooden crates built for ocean container transport.
Yes. Engineering teams accept STEP (.stp), IGES (.igs), Parasolid (.x_t), SolidWorks (.sldprt), and DXF/DWG 2D files. Rapid RFQ turnarounds are provided within 24 to 48 hours, complete with mold draft analysis, wall thickness heat maps, and process cost breakdowns.
Elevate your component performance, optimize unit costs, and secure reliable B2B supply chain execution. Send your CAD drawings, alloy specifications, and annual volume requirements to our engineering desk today.